A short drop is on the bench. The cert in the packet is for a full bar. You flip the edge of the printed cert between your thumb and index finger, scanning for the lot number match stenciled on the cut end of the drop. The band saw cut mark is still sharp, no signs of cross-contamination from other material runs earlier this shift. The part you are machining today requires tight tolerance for high-stress use, so confirming the material matches the spec is non-negotiable before you load the stock into the CNC mill vise.
Lot number cross-reference steps for this cert
Lot numbers are unique to each mill run, so even if two bars are the same alloy, mismatched lots can lead to unexpected material behavior during machining or end use, which is why this cross-reference is the first check you complete before any other prep work. The numbered steps below standardize this check so you do not miss any critical verification points:
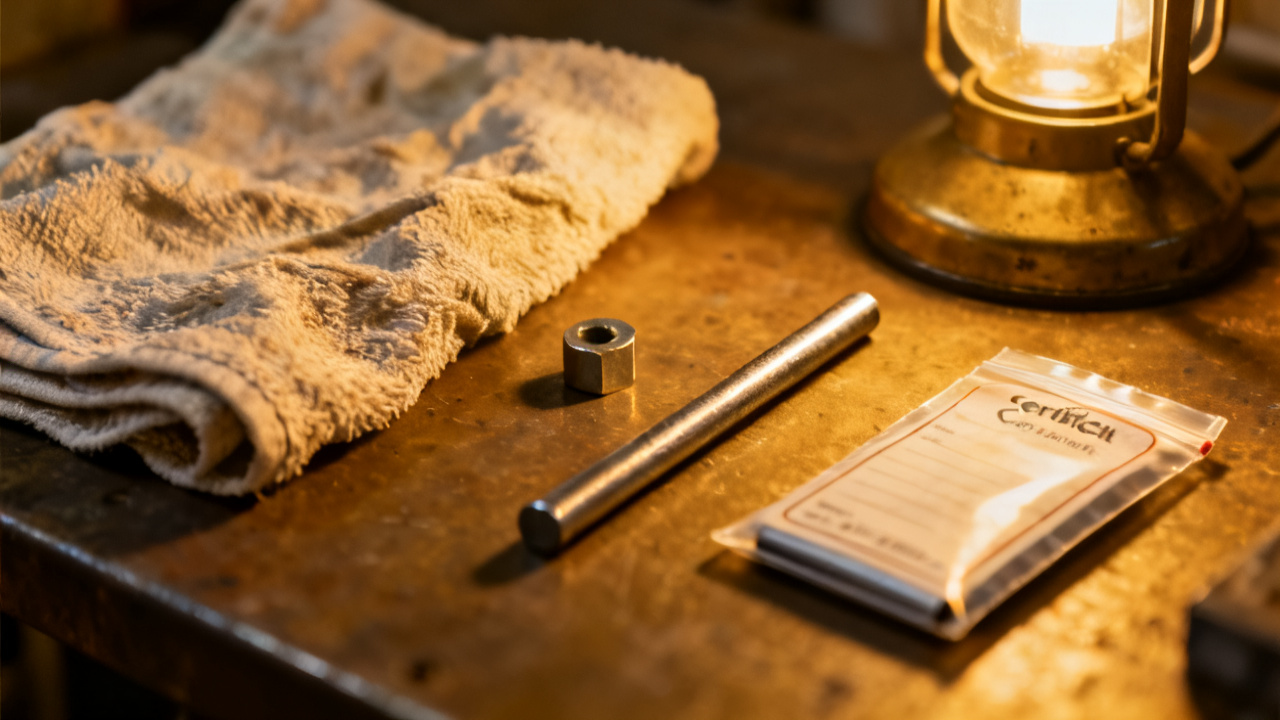
- Locate the 7-digit lot number printed in the top right corner of the cert, right below the mill’s logo.
- Compare that number to the stenciled lot on the flat end of the drop, wiping off any cutting fluid residue with a shop rag if the print is smudged.
- Cross-check the lot against the entry in the digital material tracking log for today’s production run, confirming the bar was checked into inventory two weeks prior with no outstanding quarantines.
- Note the last four digits of the lot number in the margin of the job router next to the material spec line, so downstream operators can confirm the match without pulling the full cert packet.
- Circle the lot number on the cert itself in blue permanent marker, so any future audits pull the matching document immediately.
Material property verification lines on this certification
You will find all critical mechanical properties listed in the third table on the left side of the cert, directly below the alloy composition breakdown. You confirm the tensile strength, yield strength, and elongation percentages match the requirements listed on the part print, no mill deviations are noted for those specs. You scan the heat treatment line to confirm the bar was fully annealed before shipment, which aligns with the machining parameters you loaded into the CNC mill 10 minutes ago, including the 120 SFM surface speed and 0.15 mm per tooth feed rate you set for this alloy. If any property falls outside the print’s allowed range, you flag the cert and set the drop aside for the material lead to review before you make any cuts.
Cut length validation notes for this cert packet
The cert is issued for the full length of the bar as it was shipped from the mill, so you need to confirm the drop you are using was cut from that exact bar, not a similar bar from a different lot that was mixed in during stock putaway. The cert lists the full original length of the bar it was issued for, so you cross-reference that length with the band saw cut log to confirm this drop was cut from that exact bar during last week’s rough stock prep run. Illustrative example: the full bar listed on the cert is 3660 mm long, and the drop you are using is 412 mm, cut from the bar’s leading end per the band saw run log, with the remaining stock of that bar stored in rack 4B in the raw material storage area. You measure the drop with a tape measure to confirm its length matches the cut log entry, accounting for 1.2 mm of material removed during the initial facing cut on the bar end when the full bar was first prepped for cutting. You note the drop length next to the circled lot number on the cert, so anyone pulling stock from the same bar later knows exactly how much material has been removed for this job, and can calculate the remaining usable length without pulling the entire bar from the rack.
Stamping requirements for this tracked document
Every time you access the cert to pull a drop from the associated bar, you need to add a permanent mark to confirm you completed all required checks, so there is a clear record of who accessed the document and when. You stamp the bottom left corner of the cert with the date stamp and your operator initial stamp, confirming you completed the lot, property, and length checks before beginning machining. You do not stamp over any of the mill’s printed data, as that can make the document illegible for future audits or material checks, so you leave a 1 cm margin around all pre-printed text and tables when adding your marks. You leave the original cert in the hanging job folder at Traveler Desk once you complete your notation, and keep a printed slip of the lot number and key material specs taped to the CNC machine’s control panel for quick reference during the run, so you do not have to leave the machine mid-run to cross-reference the full cert if you notice unexpected machining behavior.
Deviation notation fields on this material cert
The blank fields at the bottom of the cert are reserved for on-site notes about material use, variances, and stock levels, and you only use these fields for relevant information that pertains directly to the bar associated with the cert. If you note any minor discrepancies between the cert’s listed specs and the drop’s measured properties that fall within the engineering team’s pre-approved variance range, you document those discrepancies in the blank deviation fields at the bottom of the cert page. You include the exact measured value, the date of your check, and your initials next to the entry, so there is a clear paper trail of the variance for any future review by quality, engineering, or audit teams. You do not alter any of the mill’s original printed data on the cert, even if you believe there is a typo, instead flagging any suspected errors for the quality team to investigate directly with the mill, as altering original mill data can invalidate the cert for future use.
When you retrieve this same cert sheet for the next drop pull
This cert stays associated with the remaining stock of its original bar for the entire lifecycle of the material, so every time you pull a new drop from that bar, you will access the same sheet to complete your checks. You first check the notes you added on your previous use, confirming the lot number and remaining bar length match the drop you are pulling for the new run, and that there are no new deviation notes added by other operators who used the bar between your runs. You repeat the cross-reference steps to confirm the new drop matches the lot and material specs listed, adding a new note with the new drop length and run number next to your previous entry to track how much of the original bar has been used over time. If there are no remaining drops left from the original bar once you complete the new run, you add a “full bar exhausted” note at the bottom of the cert and file it in the completed job archive so no one tries to pull stock for that lot in the future, and to keep a full record of material use for audit purposes. If there is still usable stock left, you return the cert to the hanging job folder for the bar lot, so it is easily accessible for the next operator who needs to pull a drop from that same material run.