The sheet covers one operation. The print has many callouts. You set the last machined first piece on the polished granite surface plate next to your micrometer set, wiping a smudge of cutting fluid off the top edge before you reach for a pen. You cross-reference the operation number printed in the top right corner of the sheet against the work order taped to your CNC control panel to confirm you are referencing the right documentation for today’s 4140 steel run.
This Traveler’s Pre-Operation Validation Steps
You cross reference every pre-filled field on the sheet before you run a single part, to catch mismatches that could lead to scrapped material or rework. Confirm the material grade listed matches the bar stock you loaded into the machine, the spindle speed range aligns with the tooling you have loaded in the turret, and the operation number matches the step assigned to your station for this part number. You do not rely on verbal handoffs from the previous shift to confirm these details, since even small miscommunications can lead to hours of lost production time. The pre-operation steps you complete now prevent costly mistakes that could hold up the entire production schedule for this order, which has a tight delivery window for the end user. Complete the following steps in order, and do not move on to test cuts until all are marked as complete:
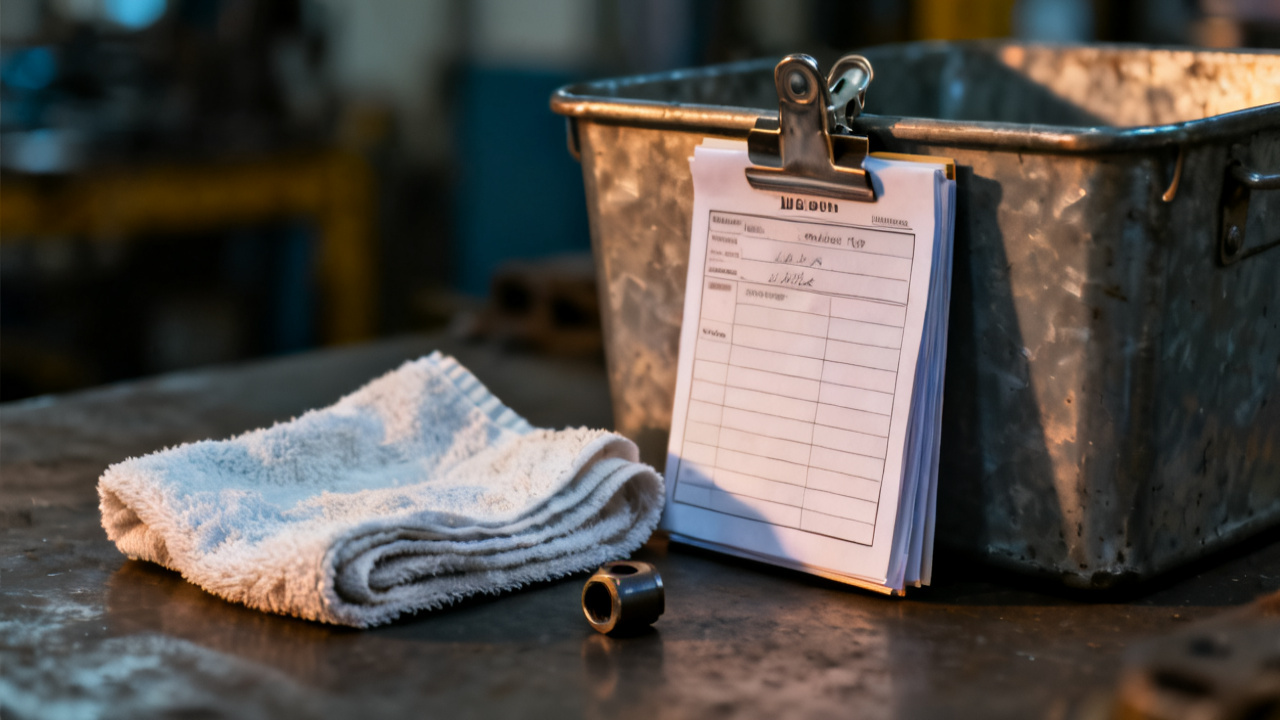
- Cross-check the part number printed on the top left of the traveler against the etched part number on the first piece of bar stock loaded in your machine chuck.
- Verify the listed tooling part numbers for each cut match the etched codes on the tools you loaded into the CNC turret at the start of your shift.
- Confirm the tolerance ranges listed for critical dimensions on the traveler align with the ranges marked on the corresponding print callouts pinned above your bench.
- Sign and date the pre-operation validation field at the bottom of the first page before you initiate the first test cut of the run.
First Piece Dimensional Verification Checks
Once the first test cut completes and you remove the part from the chuck, you let it cool to room temperature for 10 minutes before you take any measurements, to avoid skewed readings from thermal expansion of the steel. You measure every critical dimension on the first completed part before you run the rest of the batch, logging every measurement directly on the sheet in the corresponding blank field. You use calibrated measurement tools for every check, and re-zero each tool between measurements to eliminate drift that could skew your readings. You also check the surface finish of the first piece against the sample plaque provided with the work order, noting any unusual chatter marks or rough edges that could indicate a dull tool or incorrect feed rate. Illustrative example: if the listed tolerance for the through-hole inner diameter is +0.0002 / -0.0000 inches, a reading of 0.5001 inches falls within the acceptable range, while a reading of 0.4999 inches requires a tool offset adjustment before you proceed. You note any minor offsets you make to the tool path directly in the margin of the sheet, so anyone referencing the document later can see what adjustments were needed to get the first piece within spec. You do not round measurements to the nearest acceptable value, even if the difference is almost too small to see, because even a thousandth of an inch deviation can cause the part to fail final assembly checks. If any dimension falls outside the listed tolerance, you pause the run, adjust the tooling or machine settings, and run a second test piece to re-measure before you proceed to the full batch. Once all first piece measurements fall within the listed tolerances, you sign the first piece approval field on the sheet to give yourself the go-ahead to run the full batch.
Cert Entry Requirements For Completed Runs
Once you complete the full batch and confirm the final random sample checks pass all dimensional requirements, you fill out the cert fields at the bottom of the sheet with accurate, legible information. You list the exact number of good parts produced during the run, the number of scrapped parts and the reason for each scrap (tool breakage, material flaw, setup error, etc.), and the exact time the run started and ended. You do not guess at numbers for any of these fields; if you forgot to note the exact time a tool broke mid-run, you pull the log from the CNC machine control panel to get the precise timestamp instead of estimating. You also attach any calibration slips for the measurement tools you used during the run to the back of the sheet, so all supporting documentation stays paired with the traveler for the full lifecycle of the part. You make sure all entries are written in black permanent pen, so they do not smudge or fade over time as the sheet moves between departments for review and filing. If you run into questions about which fields apply to this specific operation, you bring the sheet to the Traveler Desk to get clarification from the production supervisor before you file the paperwork. Once all cert fields are filled out correctly, you place the sheet in the designated bin for finished operation documentation, where it will be picked up and reviewed by the quality control team before the parts move to the next operation.
When You Revisit This Sheet For Subsequent Batch Checks
When you pull this sheet out to reference for the next run of the same part number, you first review all the notes you added during this run, including any tool offsets, scrap reasons, or minor adjustments you made to the machine settings. These notes help you cut down on setup time for the next run, since you already know what adjustments are needed to get the first piece within tolerance on the first test cut. You cross-reference the notes on this sheet against any updated print callouts or work order changes that came in between runs, to make sure you are not relying on outdated information that no longer applies to the part’s current specifications. You add new notes directly below the existing ones for each subsequent run, so the sheet builds a complete history of every adjustment and issue encountered for this specific operation across all production runs. You do not erase or cross out old notes, even if they no longer apply, because the full history helps the engineering team identify recurring issues that can be fixed with permanent tooling or program adjustments. If you notice the same scrap reason popping up across three or more runs, you flag the sheet for the process engineering team to review, so they can evaluate if a program tweak or tooling upgrade can eliminate the issue entirely. You also use the historical measurement data logged on the sheet to spot slow drift in tool wear over time, so you can plan tool changes before they lead to out-of-tolerance parts and scrap. This accumulated data makes every subsequent run of this part faster and more efficient, reducing overall waste and keeping production on schedule for every order of this part number.